Independent equipment channel featuring HORDA machineryCase making · inner lining · collapsible boxes · frame stretching
Menu
Home / Technical guide
Technical guide

Rated speed and accepted output

Rated speed and accepted output. Control the material and process variables that affect repeatable accepted output.

Evidence-gated draft: technical facts, images and application proof require review before search indexing.
Technical guide review

Define what rated speed and accepted output must achieve.

A machine rated speed vs actual output decision starts with the real product, complete format range, material specification, accepted-output target and the operation that receives the result.

Discuss this requirement →

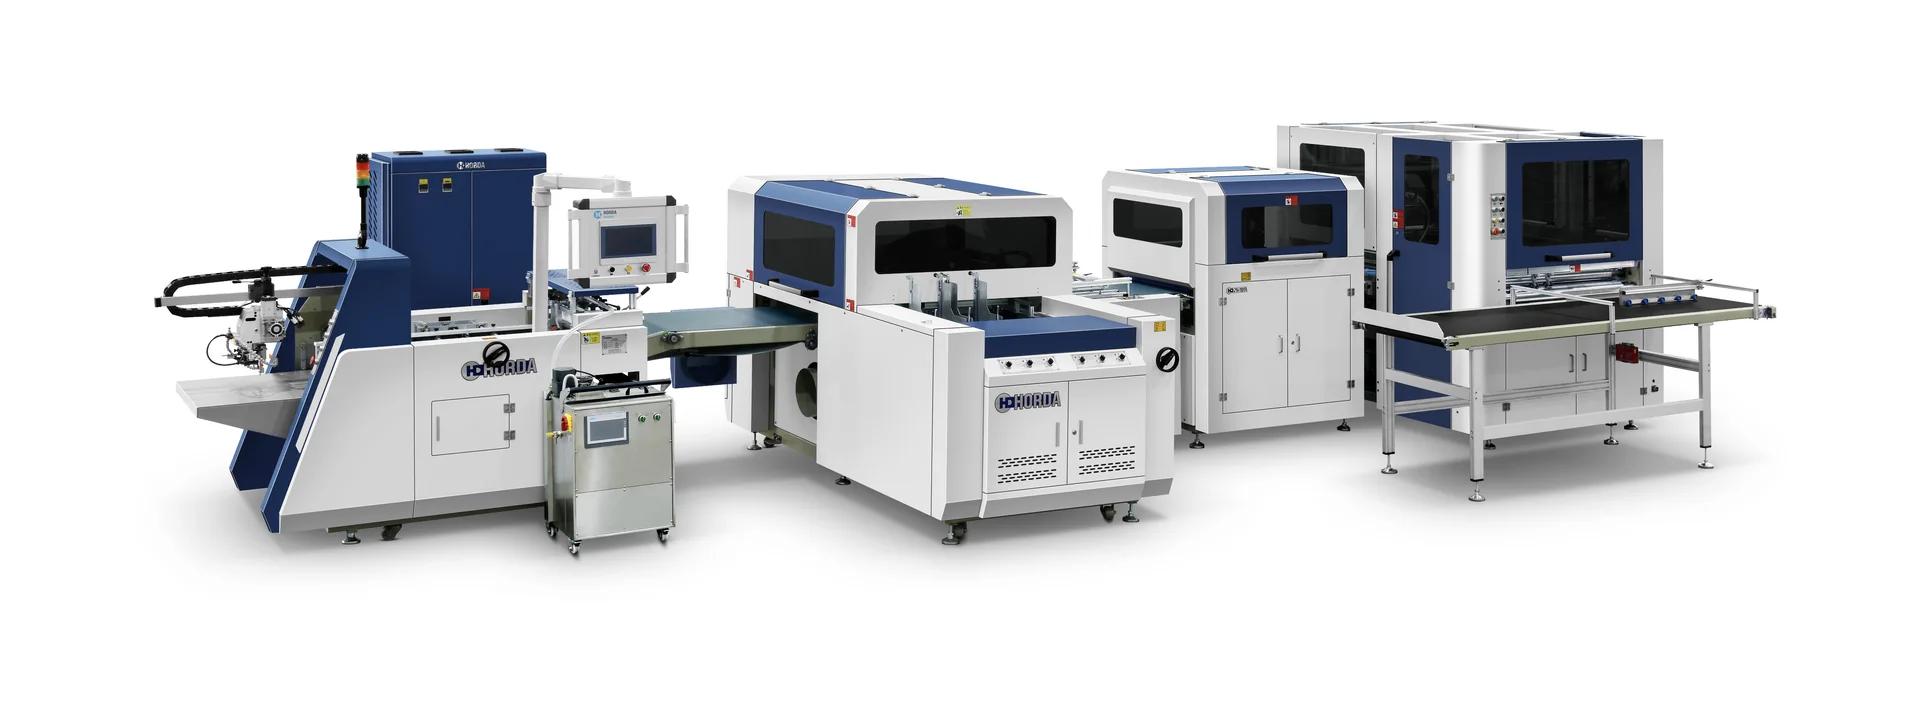
HORDA ZFM-700F/1000F automatic case making machine
Supplied visual evidence

Equipment and process references

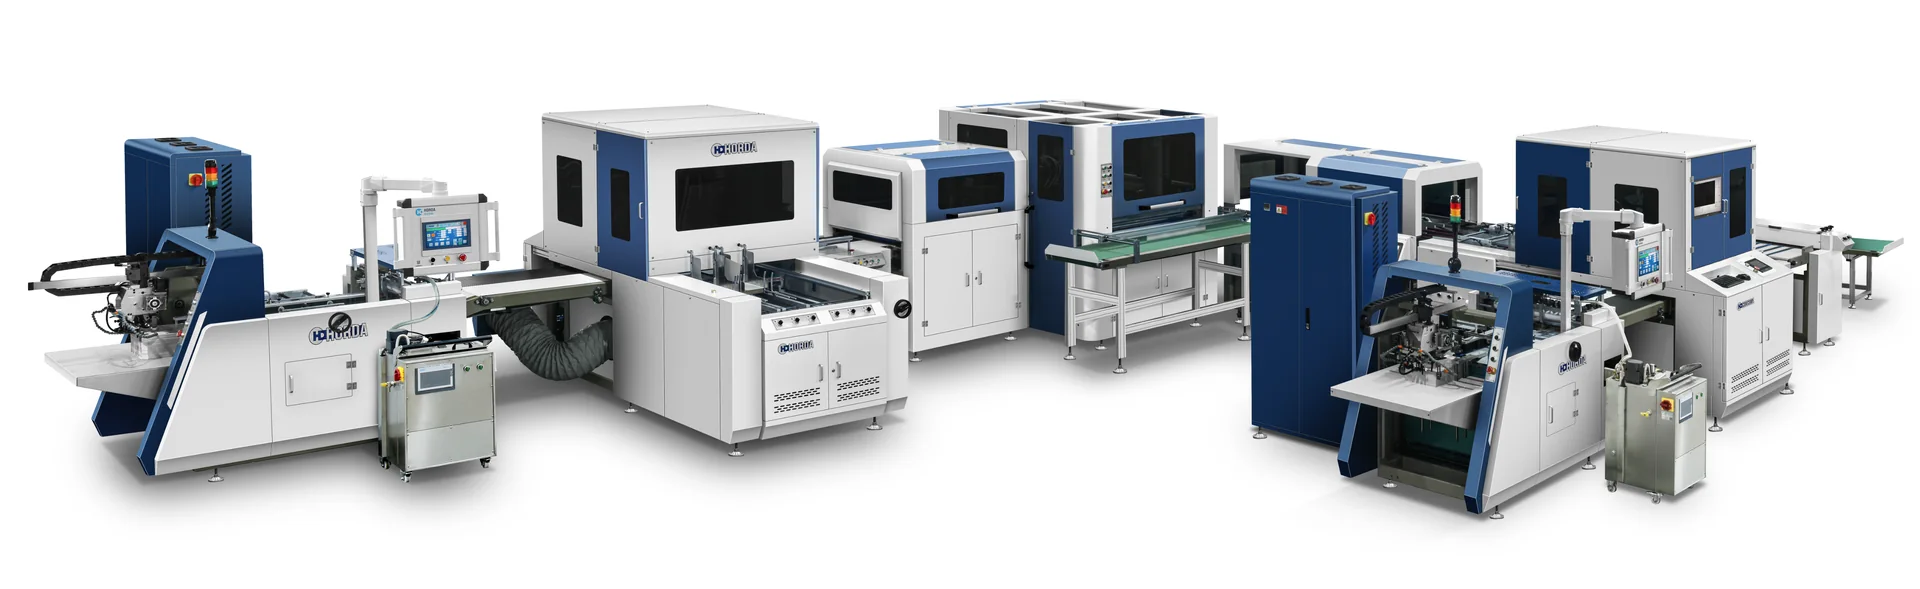
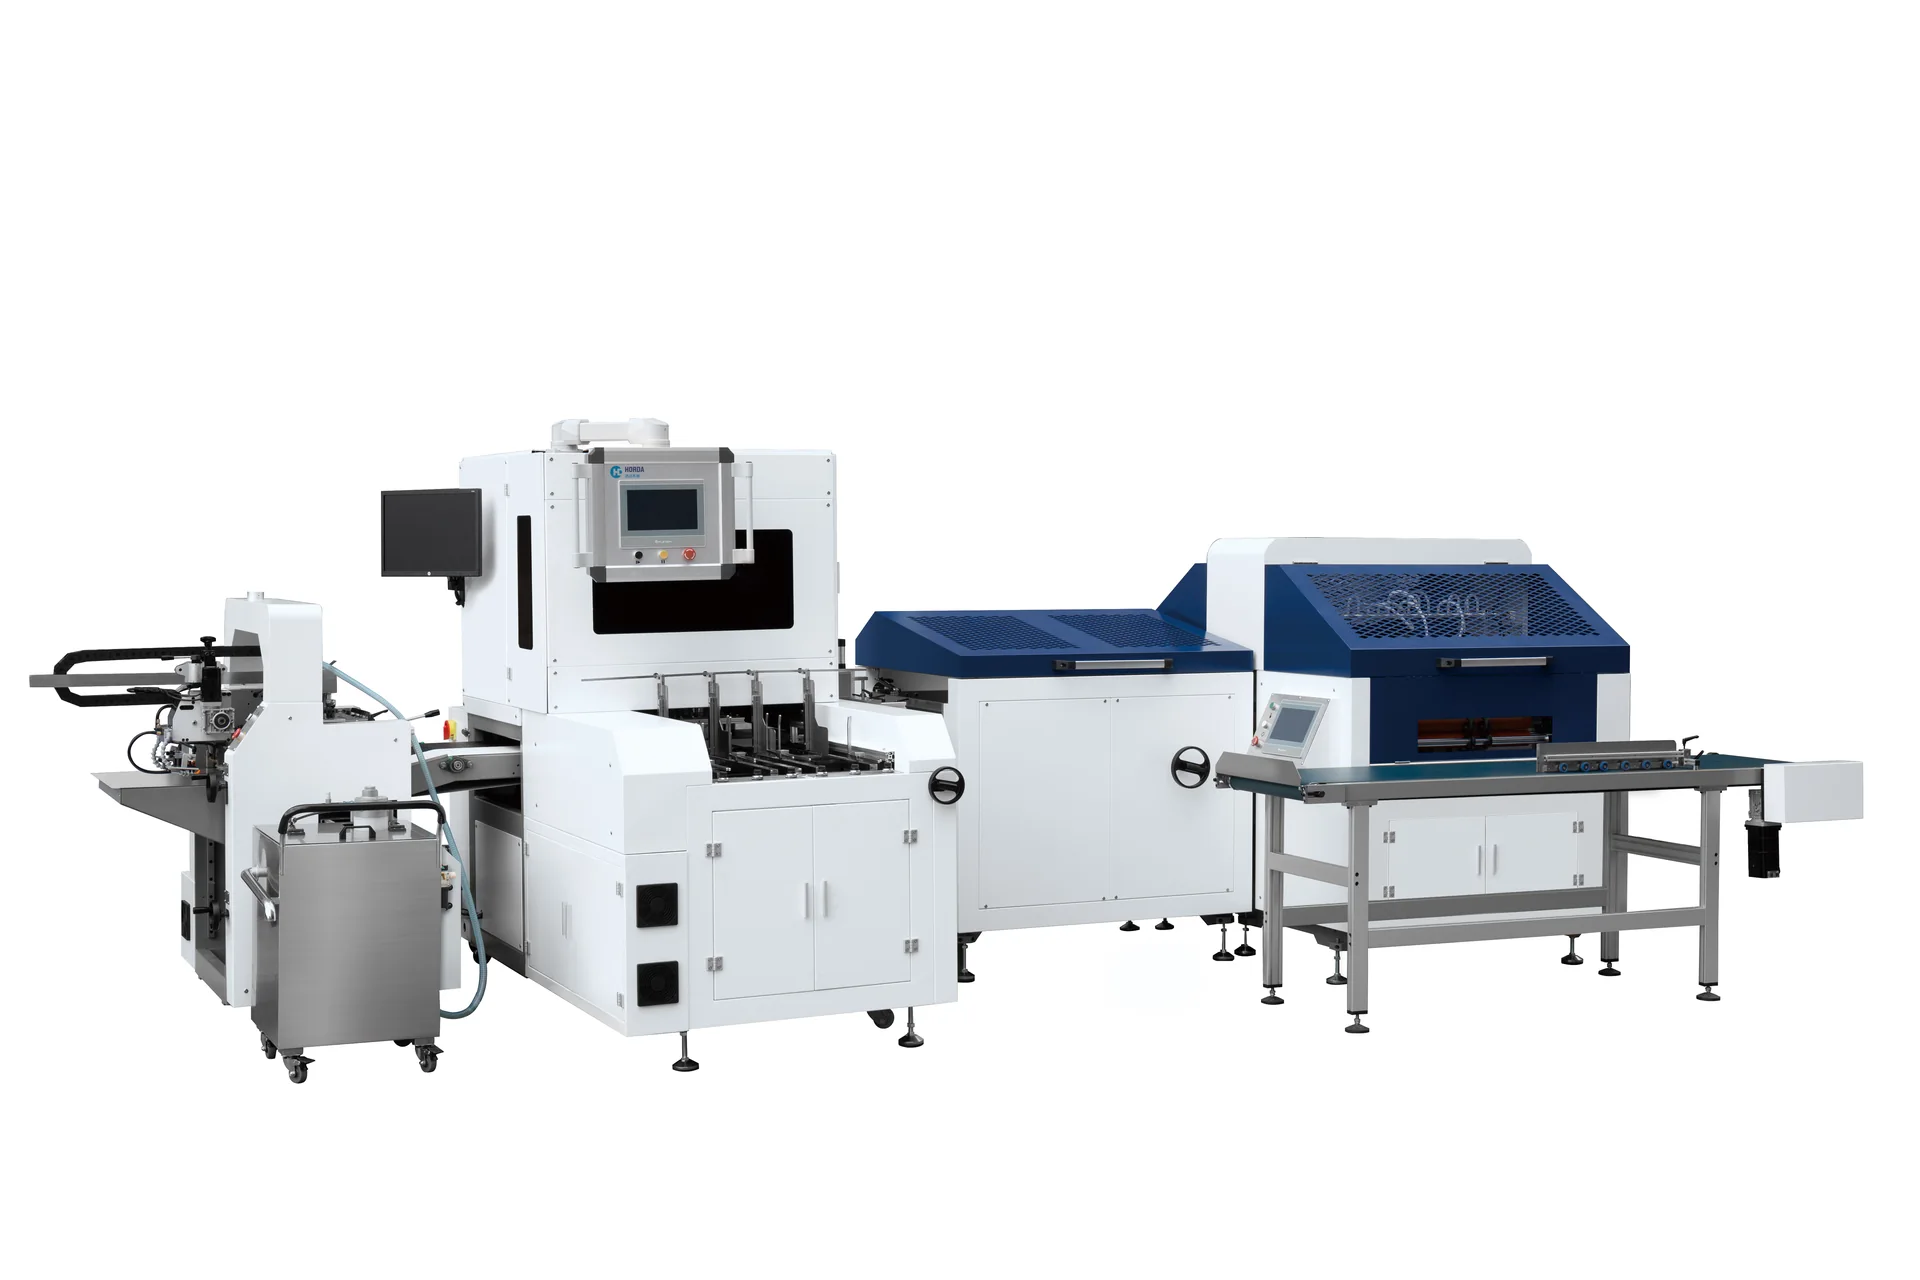
These supplied equipment images support process discussion. Confirm the exact model revision, guarding, options and configuration in the current written offer.

HORDA ZFM-700F/1000F automatic case making machine
HORDA QZFM-700E case making and inner laminating machine
HORDA ZFM-500E automatic case making machine

Image source: materials supplied for this project. Product, machine and facility identity must be confirmed against the current quotation before making a contractual claim.

Technical control plan

Use accepted pieces per hour as the capacity language.

Catalogue speed describes a machine range under stated conditions. Factory capacity includes setup, stops, rejects, inspection and the downstream bottleneck.

01Define an accepted pieceWrite the defects, dimensions and visual criteria that determine pass or reject.
02Choose representative jobsInclude frequent formats, materials and difficult printed work.
03Record productive timeSeparate running, setup, waiting, cleaning, faults and planned stops.
04Count accepted outputMeasure inspected good pieces over an agreed consecutive period.
05Balance the full lineCompare case making, lining, assembly and inspection capacity.

Variables that change the equipment decision

  • Test duration and product mix
  • Accepted-quality definition
  • Setup, downtime and rejection categories
  • Downstream bottleneck and staffing
Scope boundary: Do not multiply maximum pieces per minute by shift hours and present the result as guaranteed saleable production.
Decision framework

Three checks for rated speed and accepted output.

Use these checks to keep the machine rated speed vs actual output discussion tied to measurable inputs, outputs and responsibility boundaries.

Controlled variable

Define how rated speed and accepted output is measured during a repeatable production trial.
Reference sample

Compare changes related to machine rated speed vs actual output against one approved physical result.

Recorded outcome

Document settings, defects and accepted output when evaluating rated speed and accepted output.

Information for review

Prepare a complete machine rated speed vs actual output brief.

The six items below reduce assumptions when evaluating rated speed and accepted output and make competing technical offers easier to compare.

Variable definitionRecord this item specifically for rated speed and accepted output rather than relying on a generic machine request.
Measurement methodGive the minimum, maximum or current condition that applies to the rated speed and accepted output project.
Reference sampleAttach a drawing, photograph, specification or physical sample relevant to rated speed and accepted output.
Trial conditionsState how this rated speed and accepted output requirement will be inspected and accepted.
Defect recordExplain present production, job mix and the expected change connected with rated speed and accepted output.
Corrective actionConfirm who supplies, approves and supports this part of the rated speed and accepted output scope.
Project sequence

Move rated speed and accepted output from sample to written scope.

Keep the same product definition, material set and acceptance method throughout the machine rated speed vs actual output trial, quotation and order.

01Define the variable for Rated speed and accepted output
02Keep an approved reference for Rated speed and accepted output
03Measure current conditions for Rated speed and accepted output
04Change one factor for Rated speed and accepted output
05Record the result for Rated speed and accepted output
Frequently asked questions

Questions about rated speed and accepted output.

Use the answers as a starting checklist and confirm project-specific statements with current technical evidence.

Why does rated speed and accepted output matter?

It can change feeding stability, registration, wrapping quality, repeatability or the acceptance result for the finished component.

Can a catalogue value replace a sample trial?

No. Catalogue values screen the project; actual materials and an agreed inspection method determine practical fit.

Which variables should be recorded?

Record material specification, flat dimensions, machine settings, ambient conditions, defects, accepted output and the approved reference sample.

How should a process change be evaluated?

Change one controlled variable at a time and compare the result against the same approved sample and inspection criteria.

Primary topic: machine rated speed vs actual output. This page remains excluded from search while its facts, images and application proof are under review.

Explore next

Related planning pages.

Continue from rated speed and accepted output to the most relevant equipment, process, application or buyer-information page.

Build the right process

Ready to review your box sample?

Send the finished product, flat drawing, materials, size range and target output.

Request a quote →